Dye-Sublimation Printer
Fabric Definitions — dye and colour definitions from Apparel Search
Search Apparel Search
At a Glance
Definition: A dye-sublimation printer is a computer printer that uses heat to transfer dye onto materials such as fabric, printing a reverse image on transfer paper that a heat press then drives into polyester or other synthetic fibres as a gas.
Also known as: Dye-diffusion (the technically corrected name for the process)
Category: Fabric Definitions
Word Origin
The process was named sublimation because the dye was believed to pass directly from solid to gas without a liquid stage. That was later shown to be incorrect — there is some liquefying of the dye — and the technically correct name became dye-diffusion, although dye sublimation remains the name in general use.
A dye-sublimation printer is a computer printer that uses heat to transfer dye onto materials such as fabric. The dye-sublimation printing process is used to print on polyester or other synthetic fabrics, for applications such as T-shirts, banners, table covers, ID cards, sportswear and flags. The image is first printed in reverse on coated heat-resistant transfer paper; then, in a heat press at around 180 to 210 C (375 F), the dye turns to gas, permeates the fabric and solidifies into its fibres, so the fabric is permanently dyed and can be washed without damaging the quality of the image.
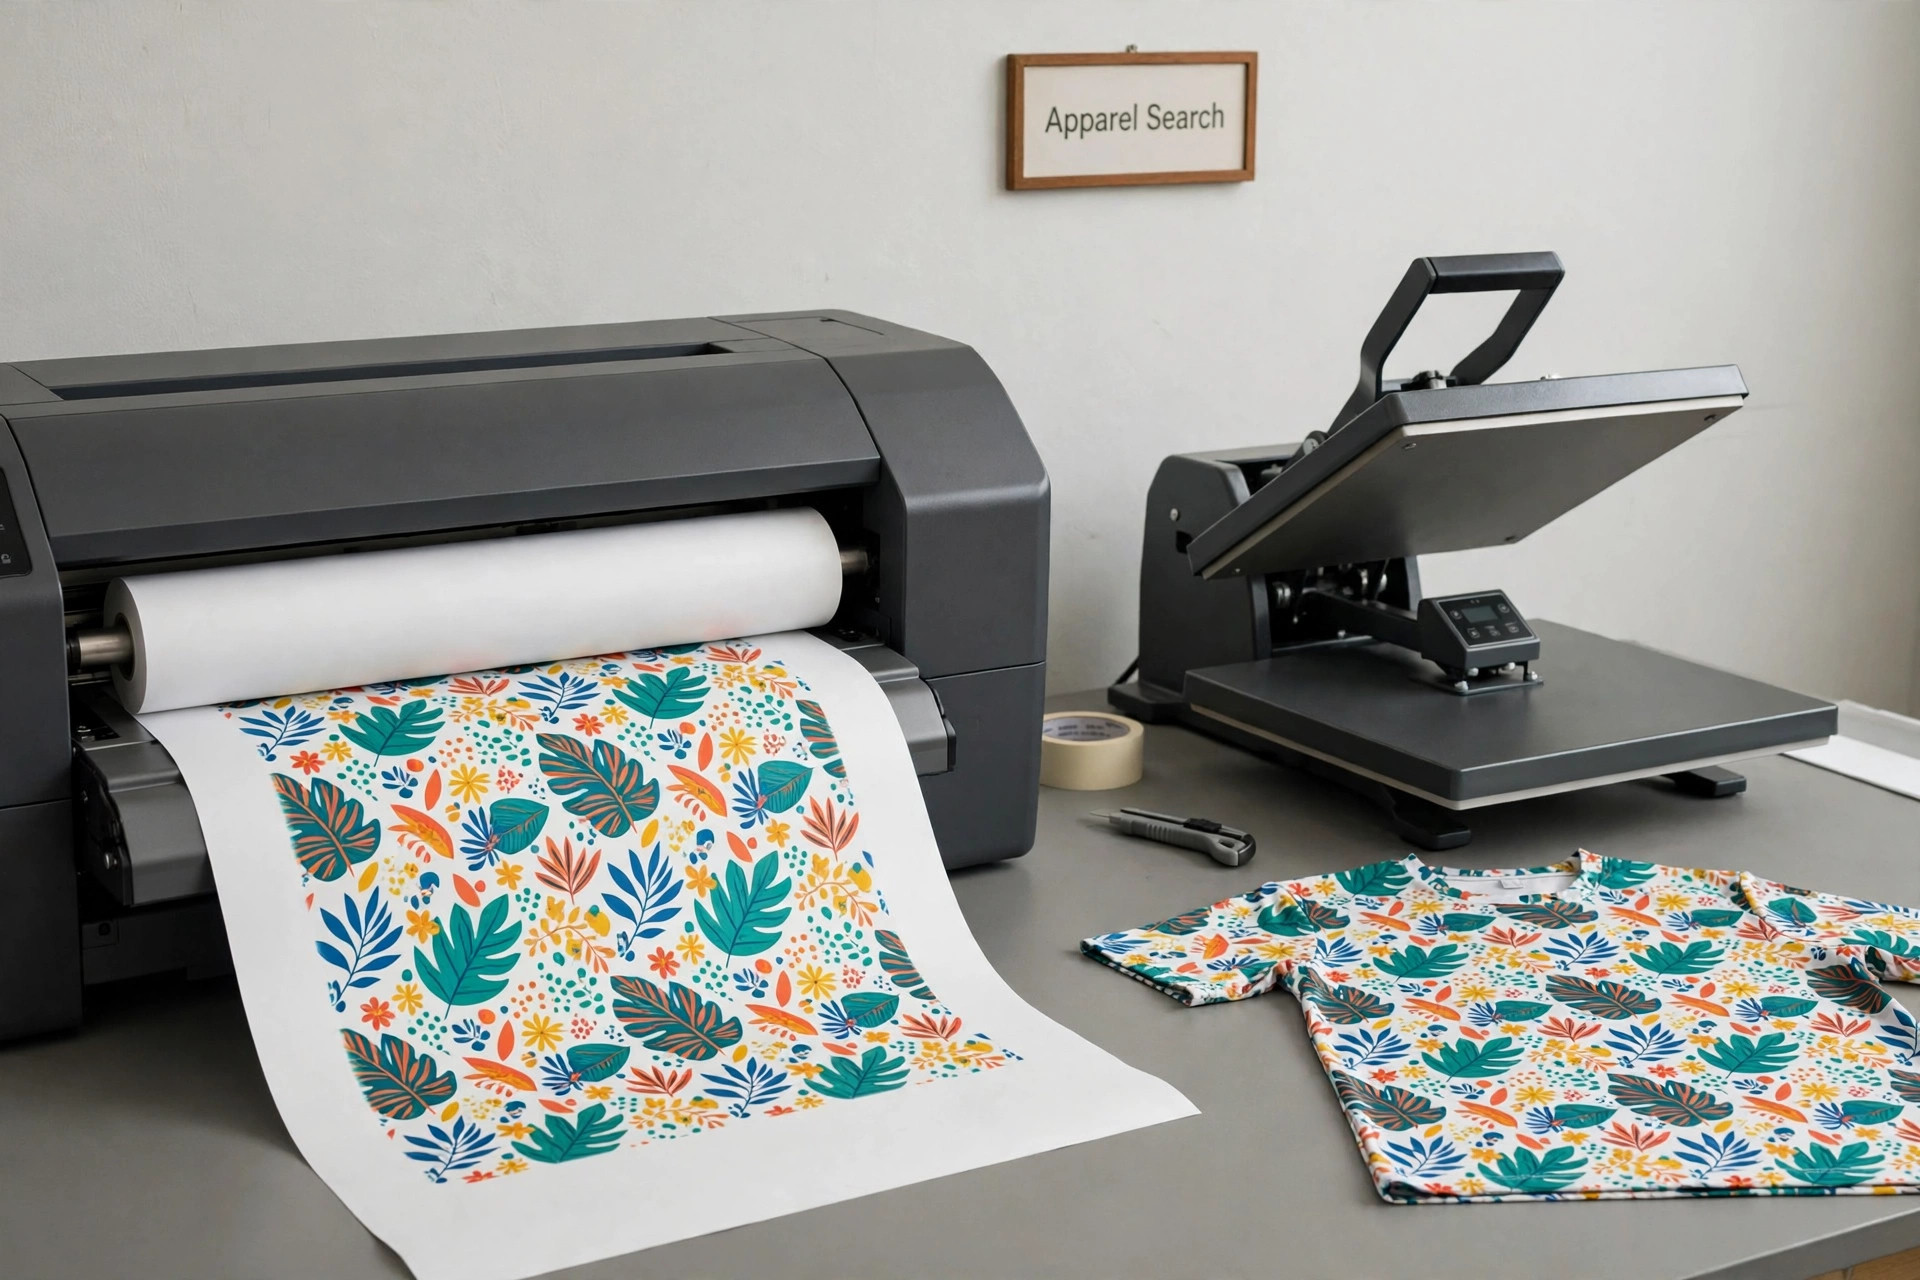
How the Transfer Works
The inks are the key to the process: dye-sublimation inks are a disperse dye suspended in a liquid solvent such as water — the same disperse class described in the dye definition. Images are printed on coated heat-resistant transfer paper as a reverse image of the final design, then transferred onto polyester fabric in a heat press operating at around 180 to 210 C (375 F). Under high temperature and pressure the dye turns into a gas, permeates the fabric and then solidifies into its fibres. Because the dye bonds to the transparent fibres of the synthetic fabric, colours can be extraordinarily brilliant, truly continuous tones equivalent to photographs can be achieved without special techniques such as half-screen printing, and the image can be printed all over the entire item, with no difficulty in printing all the way to the edges.
The name needs one correction, which the trade has never quite adopted. Sublimation was applied because the dye was considered to make the transition between the solid and gas states without going through a liquid stage; that understanding was later shown to be incorrect, as there is in fact some liquefying of the dye, and the proper name for the process became dye-diffusion. The discovery has not eliminated the original name from use in the textile or fashion industry, and most people still call the process dye sublimation. These printers are also distinct from dye-sublimation heat transfer imprinting printers, which use special inks to create transfers designed to be imprinted on textiles and in which the dyes do indeed sublimate; many consumer and professional dye-sublimation printers are designed and used for producing photographic prints.
From Toner Machines to Large-Format Inkjet
The original dye-sublimation printers were an electrostatic technology using toners. The machines used for apparel work now are generally large-format inkjet printers using specially formulated inks, printing wide transfer paper that is then matched to fabric panels or finished garments on a calendar or flatbed heat press. That two-step structure — print the paper, then press the fabric — is what makes the process so flexible for short runs: a design exists only as a digital file and a paper print until the moment it is pressed, so a shop can produce one custom jersey or a hundred banners from the same equipment without screens, plates or setup waste.
Why Sportswear Runs on Sublimation
Sportswear is the process's showcase application, because team kit is polyester, carries all-over graphics, names and numbers that change every season, and must survive hard washing. Because the dye sits inside the fibre rather than in a film on top of it, a sublimated panel has no raised print to crack, peel or block breathability, and the hand of the fabric is unchanged; the advantages over other methods of textile printing are that images are permanent and do not peel or fade, and the dye does not build up on the fabric. The same properties suit flags and banners, where colour must read on both sides of a light fabric, and table covers and ID cards, where photographic detail matters. The limits follow from the chemistry: sublimation dye is for synthetic fibre, light-coloured fabric shows the design best because the inks are transparent, and a garment that is already sewn can only be printed where the press can reach it flat — which is why all-over sublimation prints are usually pressed as cut panels before sewing. For an organiser specifying a whole kit, sublimation is one of four decoration routes, each with its own economics; the Apparel Search team uniform decoration guide compares it with screen printing, embroidery and heat-applied names and numbers.
Common Questions
What fabrics does dye sublimation work on?
Dye sublimation is used for polyester and other synthetic fabrics. The dye bonds to the transparent fibres of the synthetic fabric, which is why colours can be extraordinarily brilliant and why the process does not give the same result on untreated natural fibres.
How does a dye-sublimation print get onto the fabric?
The design is printed as a reverse image on coated heat-resistant transfer paper using disperse dye inks suspended in a liquid solvent. A heat press operating around 180 to 210 C (375 F) then transfers it: under heat and pressure the dye becomes a gas, permeates the fabric and solidifies into its fibres.
Can sublimation-printed fabric be washed?
Yes. The fabric is permanently dyed, so it can be washed without damaging the quality of the image, images do not peel or fade as surface prints can, and the dye does not build up on the fabric.