Textile Printing Machines
Miscellaneous Definitions — the intermittent and duplex machines, roller engraving, stenciling and the preparation of cloth and colors, from Apparel Search
Search Apparel Search
At a Glance
Definition: Textile printing machines are the machines that apply color to cloth in pattern at production scale — above all the engraved-roller machine and its intermittent and duplex developments — together with the roller engraving, cloth preparation and color preparation the process depends on.
Category: Miscellaneous Definitions
Many improvements have been made in printing machines, chief among them the intermittent and the duplex machines. In the intermittent machine, any or all of the rollers may be moved out of contact with the cylinder at will and at certain intervals, so bordered goods such as shawls and sarries can be printed with a wide border across their width at varying distances. The duplex, or reversible, machine prints both sides of the cloth, combining two ordinary machines so the second prints an exact duplicate of the first impression on the plain side, in such a way that both printings coincide. This page is the companion to the main textile printing definition: it covers the machines, the advantages of roller printing, stenciling, the engraving of copper rollers, and the preparation of cloth and colors on which every method depends. Roller printing also has its own page — see the roller printing definition — as does screen printing.
On This Page
Machines That Interrupt and Machines That Print Twice
The standard roller machine prints continuously, which is its strength until a design must not be continuous. The intermittent machine answers that case: any or all of the rollers may be moved out of contact with the cylinder at will, and at certain intervals. Such machines are used in the printing of shawls and sarries for the Indian market, goods which require a wide border right across their width at varying distances — sometimes every three yards, sometimes every nine yards — and it is to effect this, with rollers of ordinary dimensions, that intermittent machines are used. The body of the sarrie will be printed, say for six yards, with eight rollers; these then drop away from the cloth and others, which have up to then been out of action, immediately fall into contact and print a border or crossbar, say one yard wide, across the piece; they then recede from the cloth and the first eight again return and print another six yards, and so on continually.
The duplex, or reversible, machine derives its name from the fact that it prints both sides of the cloth. It consists really of two ordinary machines so combined that when the cloth passes, fully printed on one side from the first, its plain side is exposed to the rollers of the second, which print an exact duplicate of the first impression upon it in such a way that both printings coincide. A pin pushed through the face of the cloth ought to protrude through the corresponding part of the design printed on the back, if the two patterns are in good fit.
The Advantages of Roller Printing
The advantages possessed by roller printing over all other processes are mainly three. Firstly, its high productivity: 10,000 to 12,000 yards being commonly printed in one day of ten hours by a single-color machine. Secondly, its capacity of being applied to the reproduction of every style of design, ranging from the fine delicate lines of copperplate engraving and the small repeats and limited colors of the perrotine to the broadest effects of block printing, and to patterns varying in repeat from 1 to 80 inches. And thirdly, the wonderful exactitude with which each portion of an elaborate multicolor pattern can be fitted into its proper place, and the entire absence of faulty joints at its points of repeat or repetition — a consideration of the utmost importance in fine delicate work, where such a blur would utterly destroy the effect.
Stenciling and Its Ties
The art of stenciling is very old. It has been applied to the decoration of textile fabrics from time immemorial by the Japanese, and has found increasing employment in Europe for certain classes of decorative work on woven goods for furnishing purposes. The pattern is cut out of a sheet of stout paper or thin metal with a sharp-pointed knife, the uncut portions representing the part that is to be reserved or left uncolored. The sheet is now laid on the material to be decorated and color is brushed through its interstices.
With suitable planning an all-over pattern may be just as easily produced by this process as by hand or machine printing, and if several plates are used, as many colors as plates may be introduced into it. The peculiarity of stenciled patterns is that they have to be held together by ties — certain parts of them have to be left uncut, so as to connect them with each other and prevent them from falling apart in separate pieces. A complete circle cannot be cut without its center dropping out, and consequently its outline has to be interrupted at convenient points by ties or uncut portions. The necessity for ties exercises great influence on the design: in the hands of a designer of indifferent ability they may be very unsightly, but a capable designer utilizes them to supply the drawing, so that they form an integral part of the pattern and enhance its artistic value. For single-color work a stenciling machine was patented in 1894 by S. H. Sharp, consisting of an endless stencil plate of thin sheet steel passing continuously over a revolving cast iron cylinder, the cloth passing between the two while color is forced through the holes in the stencil by mechanical means.
Other Methods: Combinations, Surface Rollers and Lithography
Although most work is executed throughout by one or other of the five distinct processes, combinations of them are not infrequently employed. Sometimes a pattern is printed partly by machine and partly by block; and sometimes a cylindrical block is used along with engraved copper-rollers in the ordinary printing machine. The block in this latter case is in all respects, except that of shape, identical with a flat wood or coppered block, but instead of being dipped in color it receives its supply from an endless blanket, one part of which works in contact with color-furnishing rollers and the other part with the cylindrical block. This block is known as a surface or peg roller. Many attempts have been made to print multicolor patterns with surface rollers alone, but with little success, owing to their irregularity in action and to the difficulty of preventing them from warping — defects not present in the printing of linoleum, in which opaque oil colors are used.
The printing of yarns and warps is extensively practiced, usually carried on by a simple sort of surface printing machine. Lithographic printing, too, has been applied to textile fabrics with somewhat qualified success: its irregularity and the difficulty of printing all-over patterns to repeat properly have restricted its use to the production of decorative panels, equal in size to that of the plate or stone, and complete in themselves.
Engraving the Copper Rollers
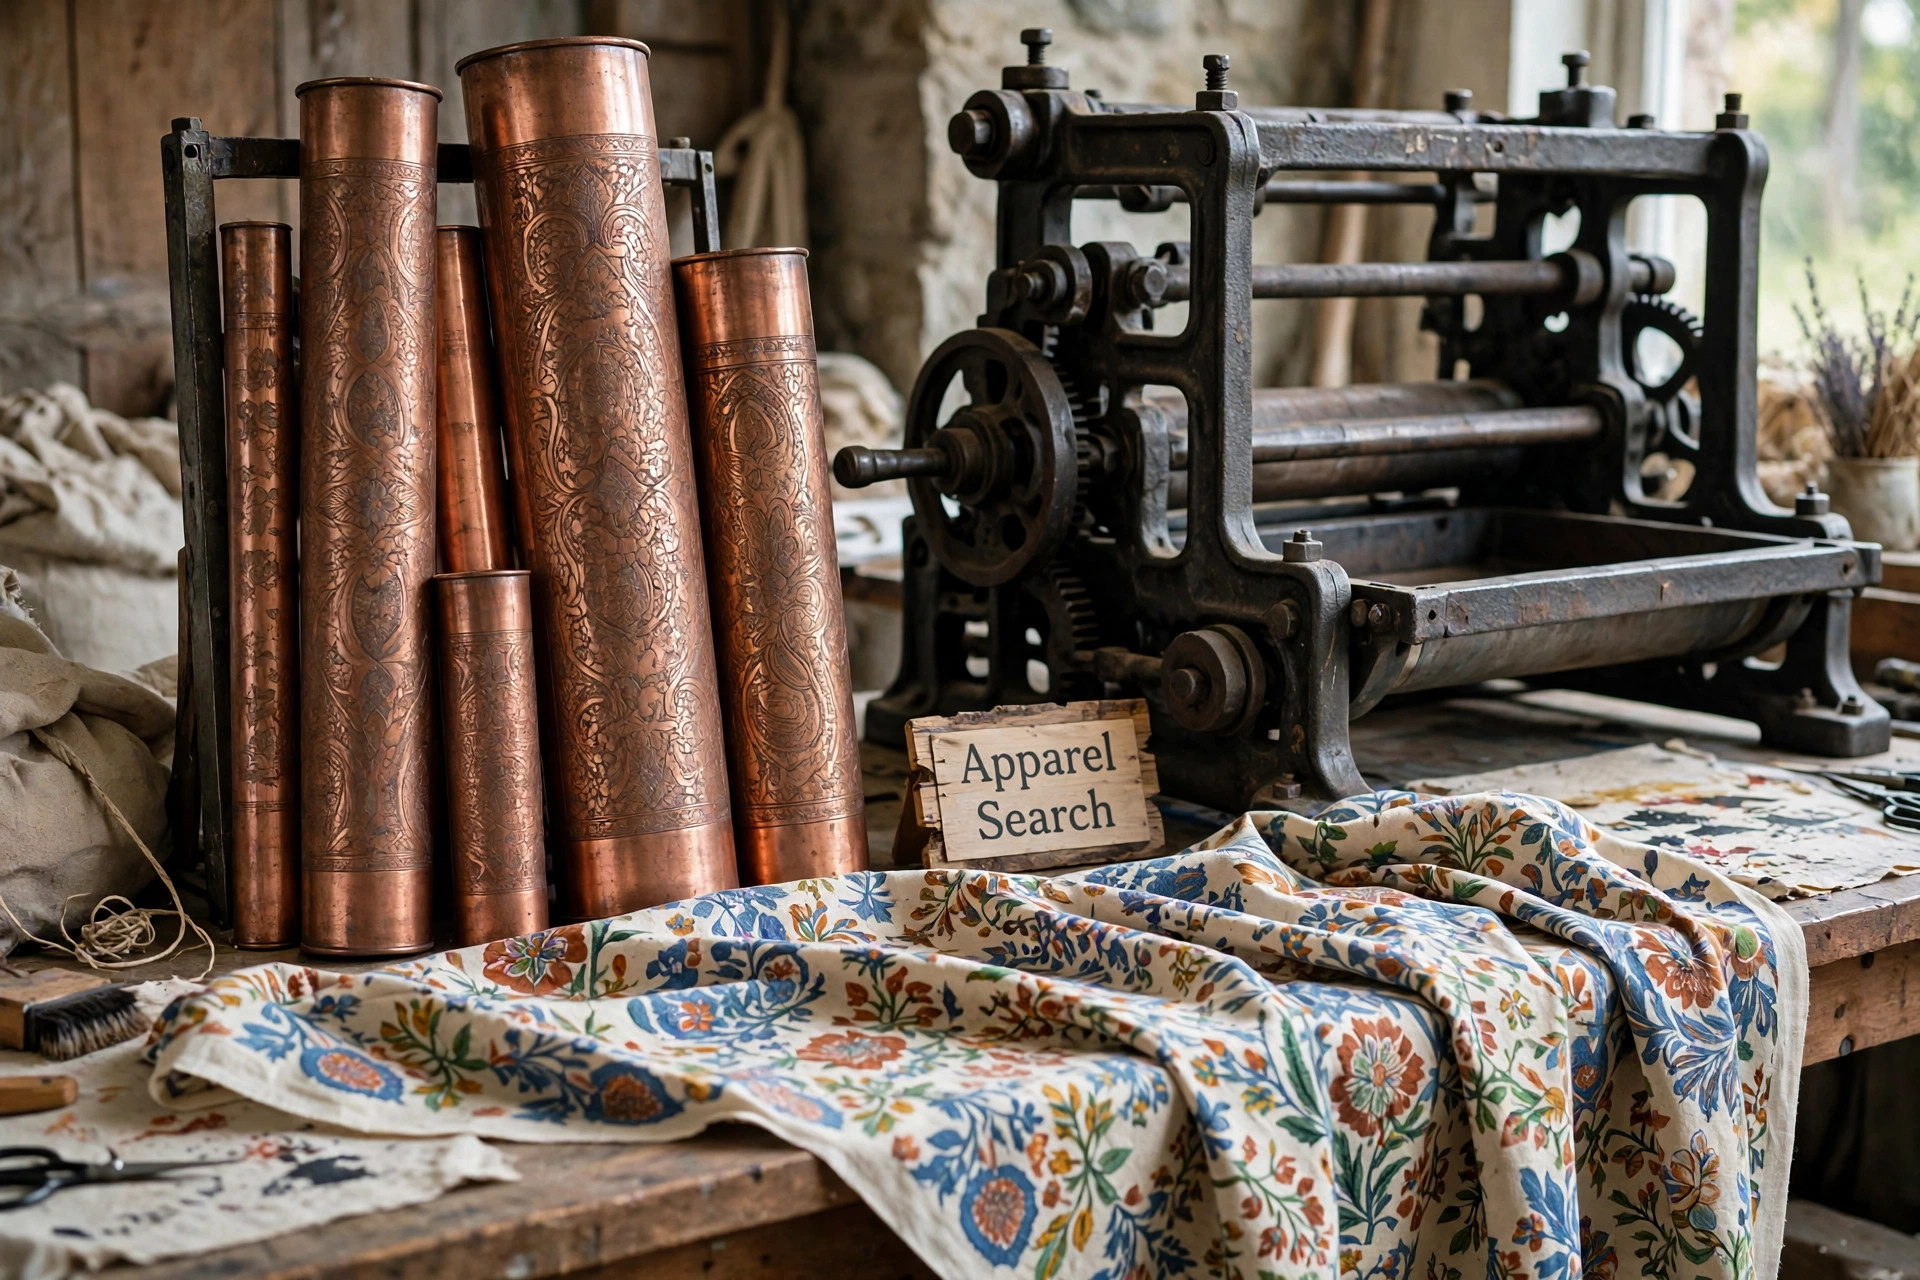
The engraving of copper rollers is one of the most important branches of textile printing, and on its perfection of execution depends, in great measure, the ultimate success of the designs. Roughly speaking, the operation of engraving is performed by three different methods: (1) by hand, with a graver which cuts the metal away; (2) by etching, in which the pattern is dissolved out in nitric acid; and (3) by machine, in which the pattern is simply indented.
Engraving by hand is the oldest and most obvious method, but the least used on account of its slowness. The design is transferred to the roller from an oil color tracing and cut out with a steel graver, prismatic in section and sharpened to a beveled point. It requires great steadiness of hand and eye, and although capable of yielding the finest results it is only now employed for very special work and for patterns too large in scale to be engraved by mechanical means. In the etching process an enlarged image of the design is cast upon a zinc plate by means of an enlarging camera and prisms or reflectors; on this plate it is painted in colors roughly approximating to those in the original, and the outlines of each color are carefully engraved in duplicate by hand. The reduction of the design and its transfer to a varnished copper roller are both effected at one operation in the pantograph machine, which can reduce a pattern from one-half to one-tenth of its size: as its stylus is moved along the engraved lines of the plate, a series of diamond points cut a reduced facsimile of them through the varnish with which the roller is covered, each color of a design being transferred in this way to a separate roller. The roller is then placed in a shallow trough containing nitric acid, which acts only on those parts from which the varnish has been scraped, the roller being revolved during the whole immersion to ensure evenness; when the etching is sufficiently deep the roller is washed, the varnish dissolved off, and any parts not quite perfect retouched by hand.
In machine engraving the pattern is impressed in the roller by a small cylindrical mill on which the pattern is in relief — an indirect process requiring the utmost care at every stage. One repeat of the pattern is first engraved by hand on a small highly polished soft steel roller, usually about 3 inches long and from half an inch to 3 inches in diameter; it is then hardened and tempered, forming the die from which the mill is made. To produce the mill, a softened steel cylinder is screwed tightly against the hardened die and the two are rotated under constantly increasing pressure until the softened cylinder has received an exact replica in relief of the engraved pattern; the mill in turn is hardened and tempered. The copper roller must have a circumference equal to an exact multiple of that of the mill, so that the pattern will join up perfectly without the slightest break in line. The mill is placed in contact with one end of the copper roller on a lever support, weights supply the pressure, and roller and mill are revolved together, the projecting parts of the mill being forced into the softer copper and engraving it in intaglio with several replicas of what was cut on the original die; when the full circumference is engraved, the mill is moved sideways to its next position, and the process is repeated until the whole roller is fully engraved.
Preparation of Cloth and Colors
Behind every method stands preparation. Goods intended for calico printing ought to be exceptionally well-bleached, otherwise mysterious stains and other serious defects are certain to arise during subsequent operations. A general prepare, employed for most colors that are developed and fixed by steaming only, consists in passing the bleached calico through a weak solution of sulfated or turkey red oil; some colors are printed on pure bleached cloth, but patterns containing alizarine red, rose and salmon shades are considerably brightened by the presence of oil. Apart from wet preparations the cloth has always to be brushed, to free it from loose nap, flocks and dust, and frequently sheared by passing over rapidly revolving knives that cut off all filaments and knots, leaving the cloth perfectly smooth and clean and fit to receive impressions of the most delicate engraving. Some figured fabrics require very careful stretching and straightening on a stenter before they can be printed with formal styles of pattern, and all cloth is finally wound into rolls of convenient size for mounting on the printing machines.
The art of making colors for textile printing demands both chemical knowledge and extensive technical experience, for their ingredients must be properly proportioned and specially chosen for the particular style of work in hand: where two or more colors are associated in the same design, each must be capable of undergoing without injury the operations necessary for the development and fixation of the others. All printing pastes, whether containing coloring matter or not, are known technically as colors. The greater number contain all the elements necessary for the direct production and fixation of the color-lake; some few contain the coloring matter alone and require after-treatments for its fixation; and others again are simply mordants thickened — a mordant being the metallic salt or other substance that combines with the coloring principle to form an insoluble color-lake, either directly by steaming or indirectly by dyeing. All printing colors require to be thickened, both to enable them to be transferred from color-box to cloth without loss and to prevent them from running or spreading beyond the limits of the pattern. The thickening agents in most general use are starch, flour, gum arabic, gum senegal and gum tragacanth, British gum or dextrine, and albumen — starch being the most extensively used of all, gum tragacanth one of the most indispensable, and albumen both a thickening and a fixing agent for insoluble pigments, coagulated by hot steam after printing to fix the colors. Before printing it is very essential to strain or sieve all colors to free them from lumps and fine sand, which would inevitably damage the highly polished surface of the engraved rollers: every scratch on the surface of a roller prints a fine line in the cloth.
Styles of Printing, and the Art's Early Evidence
The widely differing properties of the hundreds of coloring matters on the market give rise to many different styles of textile printing, which fall into four great divisions: direct printing, in which the coloring matter and its fixing agent are both applied to the fabric simultaneously; the printing of a mordant upon which the color is afterwards dyed; the discharge style; and the resist or reserve style. Silk printing calls for no special mention of method — the colors and methods are the same as for wool, except that no preparation of the material is required before printing — and silk is especially adapted to discharge and reserve effects, reserved effects being produced by printing mechanical resists, such as waxes and fats, on the cloth and then dyeing it up in cold dye-liquor.
The antiquity behind these machines is harder to pin down than the machines themselves. Printing patterns on textiles by means of incised wooden blocks is so closely related in its ornamental effects to painting, dyeing and weaving that it is almost impossible to determine from ancient records how far allusion is being made to this particular process, and its original invention must probably remain a matter of inference. Actual specimens tell more: printed stuffs have been obtained from disused cemeteries in Upper Egypt, telling of Egypto-Roman use of boldly cut blocks for stamping figure-subjects and patterns on textiles, and a fragment of printed cotton was found at Arles in the grave of St Caesarius, bishop there about A.D. 542. Pliny describes a remarkable Egyptian process in which the material, white at first, was saturated not with colors but with mordants calculated to absorb color, then plunged into a cauldron of boiling dye and removed fully colored — of various colors, according to the nature of the mordants applied, although the dye in the pan was of one uniform color. Later specimens establish that more important pattern printing on textiles had become a developed industry in parts of Europe towards the end of the 12th and the beginning of the 13th century, and medieval Rhenish monasteries have been identified as cradles of the artistic craft of ornamental block cutting. After the 14th century, increasing luxury promoted woven and embroidered stuffs and textile printing fell into neglect, until it revived three centuries later, very largely under the influence of trade importing into Europe quantities of Indian printed and painted calicoes — the revival the main textile printing definition follows into the modern print-works.
Common Questions
What is an intermittent printing machine?
In an intermittent machine, any or all of the rollers may be moved out of contact with the cylinder at will and at certain intervals. Such machines are used for shawls and sarries for the Indian market, which require a wide border right across their width at varying distances.
What does a duplex printing machine do?
The duplex or reversible machine prints both sides of the cloth. It consists of two ordinary machines combined, so the second prints an exact duplicate of the first impression on the plain side, in such a way that both printings coincide.
How are copper rollers engraved?
Engraving is performed by three methods: by hand with a graver, by etching, in which the pattern is dissolved out in nitric acid, and by machine, in which the pattern is simply indented by a small cylindrical mill carrying the pattern in relief.
What are the advantages of roller printing?
High productivity — 10,000 to 12,000 yards commonly printed in one day of ten hours by a single-color machine; capacity for every style of design, in repeats from 1 to 80 inches; and the exactitude with which each portion of a multicolor pattern can be fitted into its proper place, with no faulty joints at the repeats.
Why must printing colors be thickened and strained?
Thickening enables the color to be transferred from color-box to cloth without loss and prevents it running or spreading beyond the limits of the pattern. Straining frees the color from lumps and grit that would damage the polished surface of the engraved rollers — every scratch on a roller prints a fine line in the cloth.